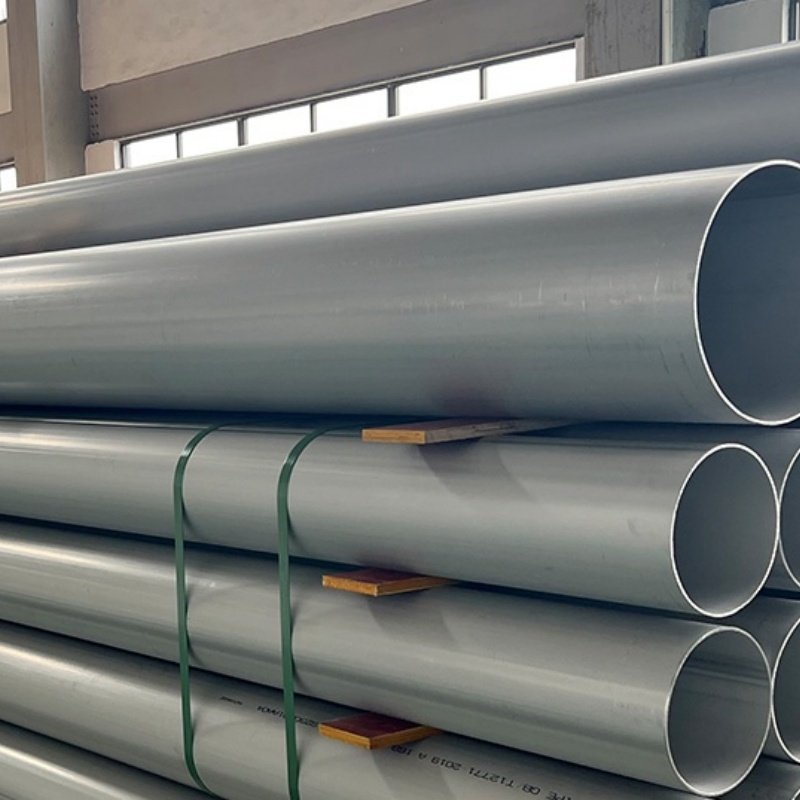
Copper-nickel 90/10 seamless pipe is supplied to
ASME SB-466 under UNS C70600. SB-466
covers seven copper-alloy UNS designations in seamless pipe and tube form,
and its Scope lists C70600 among the alloys of manufacture, to be cast as
billets of the purity and soundness suitable for processing into the
products prescribed by the specification. The matching ASTM specification
is B466/B466M.
90/10 is the workhorse copper-nickel composition. It carries about 10 %
nickel against 90 % copper, and the nickel is what makes the alloy useful
in seawater: it is the nickel that enables the adherent surface film which
protects the underlying copper. This page covers the C70600 grade; the
higher-nickel C71500 (70/30) grade is covered separately, because the
choice between them is a real engineering decision rather than a
substitution.
Copper-Nickel Grades Covered by SB-466
| Common designation | UNS number | Nickel, % | Position in the family |
|---|---|---|---|
| 90/10 | C70600 | 9.0 – 11.0 | General seawater and heat-exchanger service |
| 90/20 | C70620 | 9.0 – 11.0 | Welding-grade variant of 90/10 |
| 80/20 | C71000 | 19.0 – 23.0 | Higher-nickel, higher-strength variant |
| 70/30 | C71500 | 29.0 – 33.0 | Highest-nickel grade in the specification |
Chemical Composition (ASME SB-466, Table 1)
| Element, weight % | C70600 (90/10) | C71500 (70/30) |
|---|---|---|
| Copper, including silver | Remainder | Remainder |
| Nickel, including cobalt | 9.0 – 11.0 | 29.0 – 33.0 |
| Lead, max | 0.05 | 0.05 |
| Iron | 1.0 – 1.8 | 0.40 – 1.0 |
| Zinc, max | 1.0 | 1.0 |
| Manganese | 1.0 max | 1.0 max |
| Other named elements | — | — |
SB-466 Table 1 leaves sulfur and phosphorus as “…” for
C70600 and C71500, meaning no requirement is established for those two
elements in those grades, and it shows chromium and other named elements the
same way; the weld-grade variants C70620 and C71520 carry explicit limits
instead, with sulfur and phosphorus at 0.02 % max and carbon at 0.05 % max
listed under other named elements. SB-466 7.2.1 states that for alloys in
which copper is listed as
remainder, copper is the difference between the sum of the results of all
elements determined and 100 %. Section 7.2.2 gives the minimum copper-plus-named-elements
figure: 99.5 % for C70600, C70620, C71000, C71500 and C71520, and 99.8 % for
C72200. Section 7.2 confirms that the composition limits do not preclude the
presence of other elements, and that by agreement between the manufacturer
and purchaser, limits may be established and analysis required for unnamed
elements. Note that the iron content of 90/10 (1.0–1.8 %) is higher
than that of 70/30 (0.40–1.0 %): iron is the element most often
associated with the fouling and pitting behaviour of copper alloys in
seawater, so the tighter iron window on the higher-nickel grade is
deliberate.
Mechanical Requirements (ASME SB-466, Table 2)
| Temper | Grade | Tensile strength, min, ksi (MPa) | Yield strength, min, ksi (MPa) | Rockwell 30 T |
|---|---|---|---|---|
| O60 (soft anneal) | C70600 with C70620 | 38 (260) | 13 (90) | 45 max |
| H55 (light drawn) | C70600 with C70620 | 45 (310) | 35 (240) | 45 to 70 |
| H80 (hard drawn) | C70600 with C70620 | 50 (345) | 40 (275) | 63 min |
SB-466 8.1 lists the standard tempers as O60 (soft anneal) for pipe
generally, and the drawn tempers H55 (light drawn), H80 (hard drawn) and
HE80 (hard drawn and end annealed) for tube. Note 1 to 8.1 states that the
H55 light-drawn temper is used only where some stiffness yet capable of
being bent is needed, and that the H80 hard-drawn temper is used only when
there is a need for material as strong as commercially feasible. Table 2
note C adds that although no minimum grain size is specified, the product
must nevertheless have a fully recrystallized grain structure. Section 9.3
restricts the H80 mechanical requirements to specific size and wall-thickness
ranges and requires the requirements for other sizes to be established by
agreement, and 9.4 requires the HE80 requirements to be established by
agreement as well.
Size Range (ASME SB-466, Table X1.1)
| NPS (SPS) | OD, in. (mm) | Regular wall, in. (mm) | Extra Strong wall, in. (mm) |
|---|---|---|---|
| 1/8 | 0.405 (10.3) | 0.062 (1.57) | 0.100 (2.54) |
| 1/4 | 0.540 (13.7) | 0.082 (2.08) | 0.123 (3.12) |
| 3/8 | 0.675 (17.1) | 0.090 (2.29) | 0.127 (3.23) |
| 1/2 | 0.840 (21.3) | 0.107 (2.72) | 0.149 (3.78) |
| 3/4 | 1.050 (26.7) | 0.114 (2.90) | 0.157 (3.99) |
| 1 | 1.315 (33.4) | 0.126 (3.20) | 0.182 (4.62) |
| 1-1/4 | 1.660 (42.2) | 0.146 (3.71) | 0.194 (4.93) |
| 1-1/2 | 1.900 (48.3) | 0.150 (3.81) | 0.203 (5.16) |
| 2 | 2.375 (60.3) | 0.156 (3.96) | 0.221 (5.61) |
| 2-1/2 | 2.875 (73.0) | 0.187 (4.75) | 0.280 (7.11) |
| 3 | 3.500 (88.9) | 0.219 (5.56) | 0.304 (7.72) |
| 3-1/2 | 4.000 (102) | 0.250 (6.35) | 0.321 (8.15) |
| 4 | 4.500 (114) | 0.250 (6.35) | 0.341 (8.66) |
| 5 | 5.552 (141) | 0.250 (6.35) | 0.375 (9.52) |
| 6 | 6.625 (168) | 0.250 (6.35) | 0.437 (11.1) |
Table X1.1 is the appendix of preferred sizes, and the appendix note
states that it is recommended that wherever possible, product purchased to
this specification be ordered to the diameters and wall thicknesses indicated
in that table. The table is headed “Preferred Wall Thicknesses for
Drawn Seamless Pipe Based on SPS Diameter”, with the columns for
Regular and Extra Strong wall thickness and a set of Specials columns for
other wall thicknesses. The dimension basis is the standard pipe size
outside diameter, not a nominal bore. Wall thickness tolerances are in
Table 3 and average diameter tolerances in Table 4; the remaining tolerances,
including length, roundness, squareness of cut and straightness, are
referred by SB-466 12.4 to Specification B251/B251M, and 12.3 requires the
tolerance on distances between parallel surfaces for tubes other than round
to be agreed between the manufacturer or supplier and the purchaser.
Manufacturing Route and Heat Treatment
SB-466 6.1 requires the material of manufacture to be cast billets of the
copper alloys listed, of such purity and soundness as to be suitable for
processing into the products prescribed by the specification. Section 6.2
requires the product to be manufactured by such hot extrusion or piercing
and subsequent cold working and annealing as to produce a uniform,
seamless wrought structure in the finished product. Section 8.1.1 identifies
the O60 temper as a soft anneal, and 8.1.2 the drawn tempers. For a
seawater line that will be bent or flanged on site, the O60 condition is the
one that permits forming without a fracture risk, and the drawn tempers
exist for cases where stiffness rather than formability governs.
Inspection, Testing and Certification
- Expansion test: SB-466 10.1.1 requires tube furnished
in the O60 (soft anneal) and the HE80 (hard drawn and end annealed) tempers to
withstand an expansion to 30 % of the outside diameter when tested in
accordance with Test Method B153, with the expanded sample showing no
cracking or other defect visible to the unaided eye. Section 10.1.1.2
states that the expansion test is not required for tube furnished in tempers
other than O60 and HE80. - Flattening test alternative: SB-466 10.2 permits the
flattening test described in B968/B968M as an alternative to the expansion
test for product over 4 in. (100 mm) in diameter, and 10.2.1 requires the
flattened areas of the test specimen to be free of defects, although
blemishes of a nature that do not interfere with the intended application
are acceptable. - Nondestructive examination: SB-466 11.2.1 requires each
tube up to and including 3.125 in. (80 mm) nominal outside diameter to be
subjected to an eddy current test following Practice E243, with 11.2.1.4
requiring the notch depth standards to be 22 % of the wall thickness.
Section 11.2.1.6 allows the manufacturer to substitute the hydrostatic test
for the eddy current test for tubes above 1.25 in. (32 mm) in diameter. - Hydrostatic test: SB-466 11.2.2 requires each tube to
stand, without showing evidence of leakage, an internal hydrostatic pressure
sufficient to produce a fibre stress of 7000 psi [48 MPa], calculated as
P = 2St / (D − 0.8t) for thin hollow cylinders under tension, and 11.2.2.1 states that
the tube need not be subjected to a pressure gauge reading over 1000 psi
[7 MPa] unless specifically stipulated in the contract or purchase order.
Section 11.2.3 covers the pneumatic test at a minimum internal air pressure
of 60 psig [415 kPa] for 5 s. - Certification: SB-466 15.1 makes the test report and
certification requirements of Specification B251/B251M mandatory.
Packing & Delivery
Plastic end caps on all sizes; steel frames or wooden crates for large
diameters; VCI anti-rust wrapping. Beveled ends standard for welding; plain
ends available. Each length is marked with the standard, grade, size, heat
number and temper condition. Copper-nickel pipe is packed in a way that
protects the machined surface during handling, because the surface
condition of a copper alloy is part of its corrosion performance in
seawater.
Applications
Seawater cooling and process piping, shipboard seawater and bilge systems,
desalination plant intake, firewater and washdown systems, condensers and
heat exchangers, oil and gas production facilities, offshore platform
piping, potable and industrial water treatment piping, and pharmaceutical
and food process lines. In all of these the alloy is chosen for the film it
forms in the presence of chloride-bearing water, and for its resistance to
erosion where flow velocity is high.
Technical Notes
1. The protective film is a nickel phenomenon, and it is also the
alloy’s weakness. Copper-nickel resists seawater corrosion
because the nickel in the alloy promotes the formation of a thin adherent
surface film that protects the underlying metal, and because the alloy is
substantially more resistant to chloride pitting than copper itself. The
film is the reason 90/10 is used in seawater at all. It is also the reason
the material is not suitable for every environment: the film requires
oxygen and a controlled flow condition to develop and to repair itself, so
in fully de-aerated, stagnant or buried service the protective behaviour is
reduced. In practice the failure mode of copper-nickel in a badly designed
system is not general corrosion but localised pitting and under-deposit
corrosion where the film cannot form or cannot be repaired. Iron and
manganese contamination of the water, and deposits of corrosion products
from other materials in the same circuit, are the usual triggers.
2. The iron window in Table 1 is a corrosion specification, not a
metallurgical one. C70600 allows iron at 1.0–1.8 % while
C71500 allows only 0.40–1.0 %. That is a wide difference, and it
points in the direction of the film: iron in a copper-nickel alloy can
participate in the formation of a sulphide film in polluted or anaerobic
seawater, and iron-rich corrosion products are themselves a common source of
pitting in a copper alloy system. The higher-nickel 70/30 grade therefore
carries both a stronger intrinsic film and a tighter iron window, which is
one of the reasons the two grades are not simply a nickel-cost decision.
Note also that SB-466 7.2.2 sets the copper-plus-named-elements minimum at
99.5 % for both grades, so the balance of the analysis is a remainder
calculation rather than a directly specified value.
3. The expansion test, and the reason a hard-drawn copper-nickel
tube cannot be bent on site. Section 10.1.1 requires O60 and HE80
tube to withstand an expansion to 30 % of the outside diameter without
visible cracking, and note 8.1 states that the H55 light-drawn temper is the
one to use where stiffness is required but the product must still be capable
of being bent. The H80 hard-drawn temper, by contrast, is for material as
strong as is commercially feasible and is excluded from the expansion test
by 10.1.1.2, because it will not tolerate that deformation. This has a
direct consequence for site work: a copper-nickel line that has to be
formed, bent or re-cut in the field must be ordered in the annealed or
light-drawn condition, and a hard-drawn delivery cannot be made to fit on
site without a heat-treatment operation. Note also that 9.3 restricts the
H80 requirements to specific size and wall ranges and 9.4 requires the
HE80 requirements to be agreed in advance, so a hard-drawn enquiry needs
those points settled before the order is placed, not after.
Frequently Asked Questions
What is the ASME specification for copper-nickel 90/10 seamless pipe?
ASME SB-466 (identical with ASTM B466/B466M), which covers seamless
copper-nickel pipe and tube in UNS C70400, C70600, C70620, C71000, C71500,
C71520 and C72200. The welded form is a separate specification.
What is the difference between 90/10 and 70/30 copper-nickel?
Both are covered by SB-466 and both are copper-nickel, but they sit at
opposite ends of the nickel range: C70600 carries 9.0–11.0 % nickel
and C71500 carries 29.0–33.0 %. The higher nickel grade also carries a
lower iron range (0.40–1.0 % against 1.0–1.8 %) and a higher
strength level: in the O60 soft anneal condition C70600 requires 38 ksi
(260 MPa) tensile against 52 ksi (360 MPa) for C71500.
Which temper should I order for a seawater line that must be bent on site?
The O60 soft anneal temper, or the H55 light-drawn temper where some
stiffness is needed. SB-466 8.1 states that H55 is used where some stiffness
yet capability of being bent is needed. The H80 hard-drawn temper should
not be ordered for a line that will be formed in the field: 10.1.1.2
excludes it from the expansion test requirement, which is a direct
indication of how little deformation it will tolerate.
What certification is supplied with copper-nickel pipe?
SB-466 15.1 makes the test report and certification requirements of
Specification B251/B251M mandatory, so a full mill test report covering
chemical analysis, tensile and hardness results is issued with the
material, and EN 10204 3.1 or 3.2 certification can be provided against it.
Are the eddy current and hydrostatic tests both required?
No, they are alternatives in the way the specification is written. SB-466
11.2.1 requires each tube up to and including 3.125 in. nominal outside
diameter to be subjected to an eddy current test, and 11.2.1.6 allows the
manufacturer to substitute the hydrostatic test for the eddy current test
for tubes above 1.25 in. in diameter, with a 7000 psi [48 MPa] fibre stress
under 11.2.2.
What is the difference between C70600 and C70620?
Both are 90/10 copper-nickel. C70620 is the welding-grade variant: it
carries a higher minimum copper content of 86.5 % against the remainder
calculation of C70600, a lower lead maximum of 0.02 % against 0.05 %, and a
lower zinc maximum of 0.50 % against 1.0 %, with a carbon limit of 0.05 %
max. The tighter lead and zinc limits matter when the product will be
subsequently welded, because lead and zinc are the elements associated with
hot cracking in copper alloys.